High-Performance Orthopedic & Mobility Product Range
Certified OEM/ODM manufacturing engineered for clinical efficiency, patient stability, and seamless HCPCS/DME supply chain compliance.
Executive Whitepaper: Medical Mobility & Assistive Supply Chains in New York
As the demographic landscape of New York State continues to shift toward an aging population, the demand for durable medical equipment (DME), ergonomic folding medical walking canes, and orthopedic stabilization braces has grown exponentially. Healthcare buyers, institutional distributors, and private medical outlets in NYC face increasing pressure to secure high-quality, cost-effective, and fully certified mobility equipment.
The Greater New York area—comprising Manhattan, Brooklyn, Queens, the Bronx, Staten Island, and expanding into Long Island and Westchester County—represents one of the densest clinical procurement markets globally. With world-renowned hospital systems such as Mount Sinai, NewYork-Presbyterian, NYU Langone Health, and Montefiore Medical Center, regional outpatient rehabilitation facilities require steady, bulk supplies of mobility aids built to stringent biomechanical standards.
Demographic Drivers & Clinical Rehabilitation Needs in NY State
According to data from the New York State Department of Health (NYSDOH), residents aged 65 and older represent over 17% of the state's total population, a figure projected to approach 22% by 2030. This demographic trend directly correlates with elevated prevalence of post-stroke gait impairments, degenerative joint diseases, osteoarthritis, and total hip/knee arthroplasty recovery cycles.
Folding medical walking canes serve as an indispensable primary mobility aid during both sub-acute post-surgical discharge and long-term community ambulatory care. Their unique design—combining high tensile strength aluminum tubing, precision height-adjustment mechanisms, and quad-base dynamic pivot tips—provides urban patients with stability across diverse walking surfaces, from polished hospital floor corridors to uneven city sidewalks.
Biomechanical Engineering & Manufacturing Architecture
At BHW Medical Equipment Co., Ltd., our engineering methodology integrates high-grade metallurgical selection, ergonomic molding, and rigorous mechanical stress-testing to produce folding medical walking canes and lumbar support braces capable of handling heavy daily use. Below is an engineering overview of our folding medical walking cane production standards:
| Specification Parameter | Technical Benchmark / Engineering Standard | Clinical & Commercial Benefit |
|---|---|---|
| Primary Material Construction | Aircraft-Grade 6061-T6 Anodized Aluminum Alloy | Ensures lightweight transport (< 450g) while maintaining static load ratings up to 350 lbs (158 kg). |
| Folding Mechanism Internal Core | Heavy-Duty Dual Elastic Shock-Cord with High-Tension Bungee Insertion | Enables smooth, instant self-assembly and compact 4-fold storage for bags or urban transit. |
| Height Adjustability Range | 10-Position Dual-Pin Push-Button Lock (30" to 39" / 76cm to 99cm) | Accommodates user heights from 4'11" to 6'4", satisfying 98% of clinical patient profiles. |
| Handle Ergonomics | Contoured Soft-Touch TPR / Natural Wood / Offset Derby Grip | Reduces palmar nerve pressure and carpal tunnel strain during prolonged ambulation. |
| Base Tip & Traction | 360-Degree Swivel Anti-Slip Rubber Quad Base / Flex-Pivot Rubber Feet | Delivers multi-surface grip on slick marble, rainy sidewalks, ice, and subway platform gaps. |
| Quality Standards & Certifications | ISO 13485:2016 Quality System, CE Mark, FDA 510(k) Exemption Compliance | Guarantees seamless customs clearance and commercial distribution legality in US markets. |
Structural Integrity & Fatigue Testing Protocols
Every batch of medical walking canes manufactured at our facility undergoes static vertical compression testing, cyclic bending fatigue testing (over 100,000 stress cycles), and salt-spray corrosion testing. This guarantees long-term durability when exposed to aggressive de-icing chemicals commonly applied to New York streets during winter months.
Localized Application Scenarios across New York Metropolitan Area
Urban mobility equipment must adapt seamlessly to the dynamic lifestyle and structural environment of New York City. BHW Medical's folding walking canes and orthopedic products are engineered specifically to solve localized challenges encountered by patients navigating New York.
NYC Public Transit & MTA Subway Navigation
Commuting via MTA subways, buses, and Long Island Rail Road (LIRR) requires rapid folding capabilities. Our canes collapse into 4 compact segments under 11 inches, fitting easily into commuter bags when seated on crowded trains.
Post-Acute Outpatient Rehab & Hospital Discharge
Distributors supplying orthopedic surgical centers in Manhattan and Queens benefit from pre-packaged, ready-to-issue cane kits complete with wrist straps and carrying clips, streamlining patient discharge protocols.
All-Weather Outdoor Terrain & Winter Traction
New York winters introduce slush, black ice, and wet concrete. Our quad-base rubber tips utilize self-draining tread patterns and cold-resistant synthetic compounds to maintain flex and grip down to -15°C.
Compact Living Space & Residential Storage
High-density living in Manhattan and Brooklyn apartment buildings means space is at a premium. Self-standing quad-base designs prevent canes from slipping onto floors in small residential quarters.
Institutional Senior Care & Assisted Living Facilities
Long-term care facilities throughout Westchester and Staten Island require color-coded, durable mobility canes with anti-bacterial handle coatings to maintain safety and hygienic standards.
Ergonomic Orthopedic Spinal Support Integration
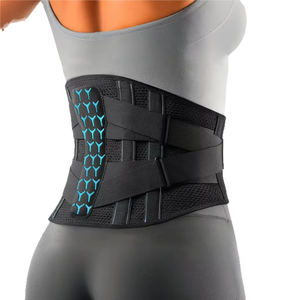
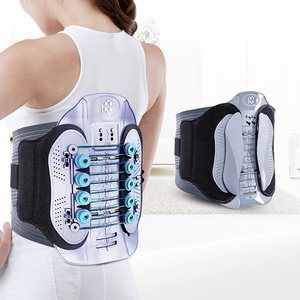
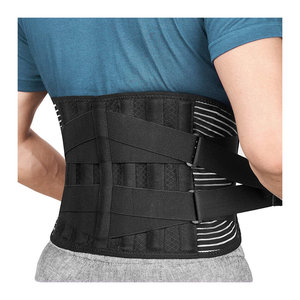
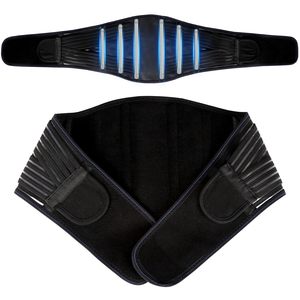
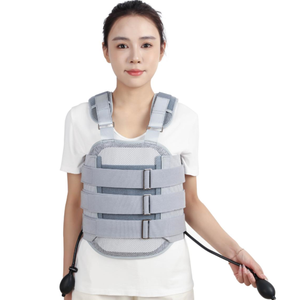
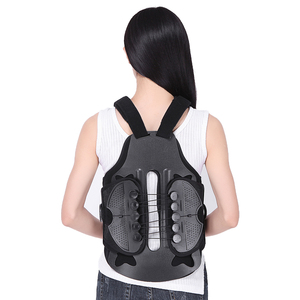
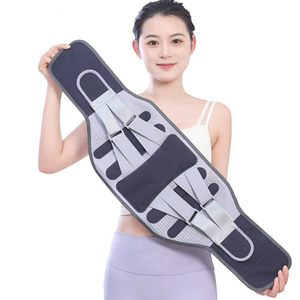
Combining walking cane assistance with dynamic lumbar support braces (such as our 3D Knit Double-Pull Belts) creates a holistic mobility solution for patients recovering from sciatica and disc herniations.
Strategic Procurement Trends in the New York DME Market
Medical equipment importers, B2B wholesalers, and institutional procurement officers in New York are navigating several key supply chain shifts:
1. Transition to Private-Label (OEM) Brand Building
New York regional medical supply distributors are increasingly opting for customized OEM branding. By adding custom laser-etched logos, retail box packaging, and localized instruction manuals directly at the China factory level, distributors enhance brand equity and command higher gross profit margins.
2. Demand for Multi-Functional & Biomimetic Ergonomics
Modern ambulatory care emphasizes products that combine style with clinical function. Features like integrated LED headlights in cane handles, biomimetic shock-absorbing pads, and 3D breathable knit fabrics in back supports are rapidly replacing outdated, industrial-looking designs.
3. Streamlined Logistics via Port of NY/NJ
B2B importers prioritizing fast turnaround favor direct ocean freight routes into Maher Terminal or Elizabeth Port in New Jersey. Factory-direct packing efficiency—maximizing master carton cubic volume—dramatically lowers sea shipping freight per unit.
4. HCPCS Code & Insurance Billing Alignment
DME suppliers servicing Medicare and Medicaid beneficiaries require strict dimensional and load-bearing compliance to match billing descriptions under HCPCS Code E0100 (Single point cane) and E0105 (Quad cane), safeguarding against audit clawbacks.
Frequently Asked Questions for NYC Procurement Officers
Detailed technical, regulatory, and commercial responses regarding factory sourcing, shipping, and customization.
We provide full compliance documentation required by U.S. Customs and Border Protection (CBP) and the FDA, including: ISO 13485:2016 Quality Management System Certificate, CE Declaration of Conformity, FDA Device Establishment Registration, Medical Device Listing numbers, Bill of Lading (B/L), Commercial Invoice, Detailed Packing List, and Certificate of Origin (Form A or COO).
Our standard MOQ for applying custom laser-etched logos or brand silk-screening on walking canes and back braces is 200 pieces per item. For custom full-color retail artwork printing boxes, our baseline standard is 500 units per packaging batch.
Sample requests are dispatched within 5 to 7 days via air express (DHL/FedEx/UPS), arriving in New York within 3 to 5 business days. Bulk ocean freight production requires 30 to 35 days, with ocean transit from Ningbo/Xiamen Port to Port of New York/New Jersey taking approximately 25 to 30 days depending on carrier service (all-water vs overland intermodal).
Yes. Our non-skid TPR and rubber quad tips are friction-tested according to ISO 11199-1 standards for static and dynamic friction coefficients. They feature internal metal washer reinforcements to prevent the aluminum shaft from wearing through the rubber base under repeated impact.
Absolute flexibility is provided for institutional orders. Buyers can mix folding walking canes, cervical collars, knee supports, cam walker boots, and spinal back braces into a single 20ft or 40ft HQ container to optimize freight volume and inventory management.
We enforce a strict 3-tier Quality Assurance System: (1) Incoming Quality Control (IQC) testing raw aluminum, elastic shock cords, and fabrics; (2) In-Process Quality Control (IPQC) monitoring assembly lines; and (3) Final Quality Control (FQC) conducting random AQL 2.5 inspections before loading master cartons.
BHW Medical Equipment Co., Ltd. — Your Trusted Manufacturing Partner
BHW Medical Equipment Co., Ltd. is a premier, certified medical device manufacturer specializing in high-grade orthopedic supports, cervical care, spinal stabilization braces, and mobility aids for international healthcare channels.
20+ Years Manufacturing Mastery
Over two decades of dedicated production experience supplying hospital groups, DME networks, and orthopedic brand owners worldwide with consistent high quality.
Global Quality Certifications
Operates under rigorous ISO 13485:2016 management standards. Products hold full CE certification and FDA compliance for smooth clearance across North America and Europe.
Full OEM & ODM Engineering
From custom aluminum extrusion tooling and plastic injection molds to specialized fabric knits and private packaging, our in-house engineering team turns technical drawings into mass production.
Request Wholesale Pricing & Factory Specifications
Partner with China's leading exporter of folding medical walking canes and orthopedic stabilization devices. Direct factory pricing, fast sample dispatch, and dedicated institutional support for New York distributors.